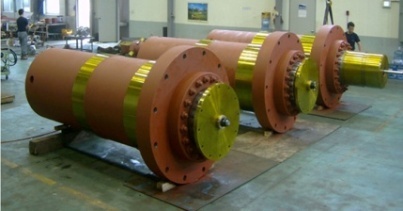
Manufacture and repair with plating, grinding and testing under the same roof. High-quality material and tight practice give long cylinder service life and lower operating cost.
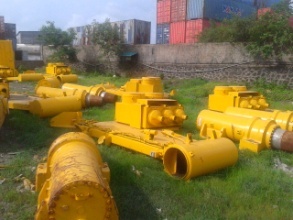
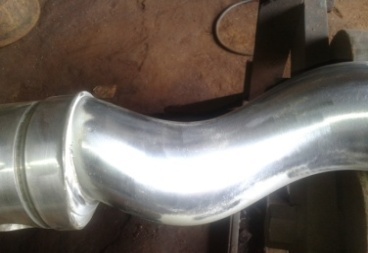
Most cylinders arrive scored, leaking or bent. We strip and assess first and quote against what we find, not against a guess — then the rod is machined, re-chromed, ground and honed back to size before the unit is reassembled with new seals and pressure tested.
Because the chrome bath, the grinders and the test rig are all ours, a rebuild does not sit in three separate queues at three separate suppliers.
Capability
Scope
Manufacture & repair
Max rod / bore length
11 000 mm
Max plating diameter
Ø 750 mm
Max grinding diameter
Ø 600 mm
Hard chrome plating
In house
Grinding & honing
In house
Pressure testing
In house
The route — five stages
01Strip & assess
Dismantled, measured and quoted against actual wear.
02Machine
Rod and bore turned true; damaged sections cut back.
03Hard chrome
Deposit laid on oversize, ready to be brought back to size.
04Grind & hone
Ground to drawing dimension and honed to finish.
05Assemble & test
New seals fitted, unit pressure tested before dispatch.

 02
 03